
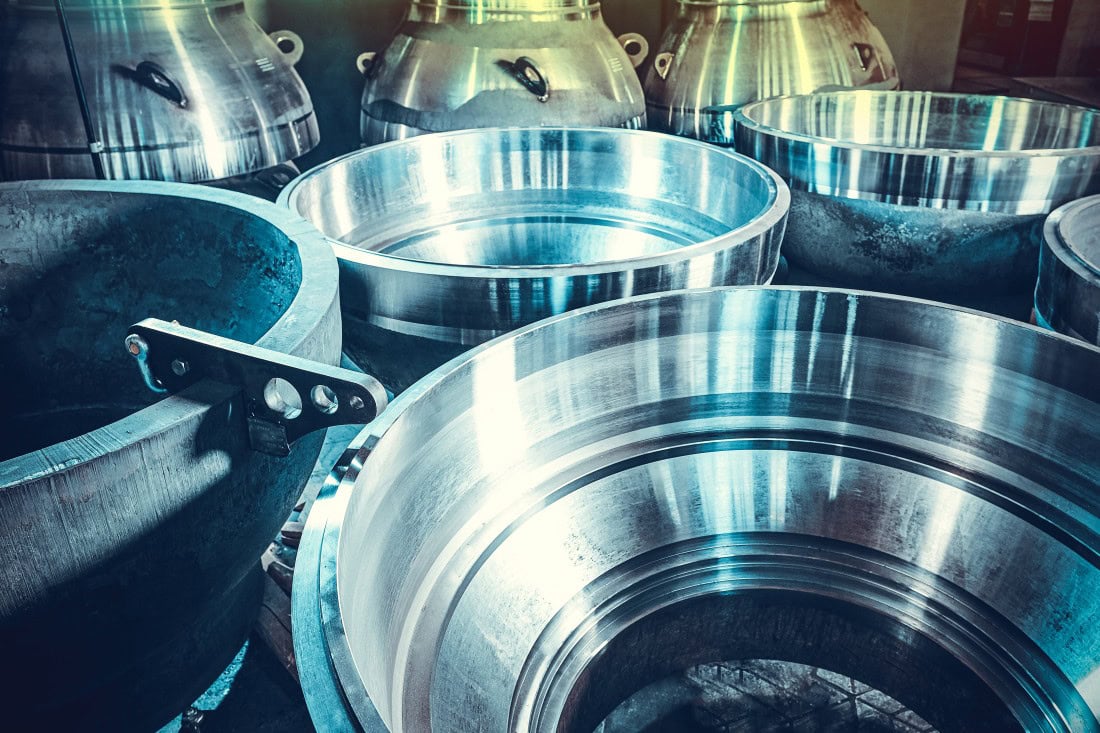
At first glance, a polished stainless steel vessel may appear to be a cosmetic upgrade. In reality, surface finish plays a critical role in equipment performance, product quality, and sanitation.
In food processing, beverage manufacturing, pharmaceuticals, and chemical production, the finish on a stainless steel vessel directly affects cleanability, corrosion resistance, contamination risk, and long-term equipment life.
This article breaks down why polished stainless steel vessels are the industry standard for hygienic processing environments, what the finish grades actually mean, and what to nail down before you specify sanitary stainless steel tanks or other custom metal process equipment.
What “Polished” Actually Means on a Stainless Steel Vessel
“Polished” is not a finish level you eyeball on the shop floor. It’s a measured spec, and it’s the difference between a vessel that passes a sanitary audit and one that doesn’t.
That distinction matters more than it sounds like it should. Two shops can hand you a tank that looks identical under the same lighting, and only one of them can provide documentation showing the surface actually meets the Ra number specified in the spec.
Surface Finish Is Measured, Not Judged by Eye
Surface finish is quantified as Ra (roughness average), expressed in microinches or micrometers. A lower Ra means fewer microscopic peaks and valleys on the surface, and fewer places for residue, bacteria, and cleaning chemicals to hide. Two vessels can look equally shiny under shop lighting and still differ by a wide margin in Ra, which is exactly why finish specs exist independently of visual inspection.
Why the Passive Layer Depends on the Finish
Stainless steel resists corrosion because chromium in the alloy reacts with oxygen to form a passive chromium oxide layer on the surface. That layer self-heals when the metal is scratched, but only if the surface conditions allow it.
A rough or contaminated surface interrupts the passive layer’s ability to reform evenly, which is how a “stainless” vessel ends up with pitting or staining anyway.
The Regulatory Baseline: What 3-A and the FDA Actually Require
Compliance on a sanitary vessel isn’t a matter of interpretation.
It’s a specific number, set by 3-A Sanitary Standards, Inc., and a set of design requirements written directly into federal food manufacturing regulations.
The 32-Microinch Rule
3-A Sanitary Standards call for product-contact surfaces to have a maximum roughness of 32 microinches (0.8 micrometers Ra). That threshold isn’t arbitrary; surfaces rougher than that retain microbial populations even after a standard clean-in-place cycle, which defeats the point of a sanitary design from the start.
What the Federal Code Actually Says
The FDA’s Current Good Manufacturing Practice regulations don’t cite a Ra number directly, but they do establish the underlying requirement that such a number exists.
Under 21 CFR 117.40, food-contact surfaces “must be corrosion-resistant when in contact with food,” and seams “must be smoothly bonded… to minimize accumulation of food particles.” A 3-A-compliant finish is how a fabricator satisfies that federal requirement in practice, not just on paper.
The Step Most Guides Skip: Passivation
Polishing and passivation are two different steps, and treating them as one is a common mistake. Polishing shapes the surface. Passivation is a chemical treatment, typically a citric acid or nitric acid bath, that removes free iron left behind by fabrication and allows the chromium oxide layer to rebuild uniformly across the entire surface, including weld zones.
A vessel that’s been ground and polished but never passivated can still corrode prematurely at the welds, which is usually where the first customer complaint originates.
Reading the Finish Grades Like a Fabricator Does
Not every application needs a mirror finish, and over-specifying polish adds cost without adding function. Three finishes cover most sanitary work.
2B Mill Finish: The Starting Point, Not the End Point
2B is the dull, as-rolled finish stainless steel that it carries when it leaves the mill. It’s economical, but its Ra typically runs too high for direct food contact, so it’s a starting material, not a finished spec.
No. 4 Finish: The Sanitary Default
A No. 4 finish is a brushed, satin surface that meets the 32-microinch 3-A threshold for most food-contact applications. It’s the most commonly specified finish for sanitary tanks because it balances cleanability, cost, and durability better than either 2B or a full mirror polish.
Electropolish: When 32 Microinches Isn’t Smooth Enough
Electropolishing uses an electrochemical process, rather than mechanical abrasion alone, to remove surface material at a microscopic level. It typically achieves Ra values well below the 3-A minimum, which is why it’s the standard in pharmaceutical and biotech applications where the process tolerance for contamination is effectively zero.
Where the Finish Actually Gets Made or Broken
A finish spec on a drawing is only as good as the fabrication process behind it. Every step between raw plate and finished vessel either protects that spec or works against it, and there’s no single step where a shortcut goes unnoticed later.
That’s the part a lot of quotes don’t account for. A vessel can be cut, welded, and formed by a shop that treats finishing as the last step instead of a requirement built into every prior one.
Laser Cutting Sets the Foundation
Laser cutting produces a clean, precise edge with a narrow heat-affected zone, which means less grinding and rework before polishing even starts. It also holds tighter tolerances on the ports, nozzles, and access points a vessel needs for fittings, agitators, and heating jackets.
Welding Is the Highest-Risk Step
Every weld has to be ground flush and re-polished to match the surrounding base metal, or it becomes a crevice where product and cleaning solution collect. Heat from welding can also disrupt the chromium oxide layer right at the weld, which is exactly why passivation after welding matters as much as the welding process itself.
Forming and Machining Round Out the Build
Rolling and forming a shell or dishing a head introduces its own stress into the material, and those zones need the same finishing attention as a weld seam. Machining the fittings, nozzles, and flanges to the correct tolerance is what lets gaskets seal properly for years instead of becoming a maintenance callback in year two.
Where Polished Stainless Steel Vessels Actually Get Used
The industries that specify polished stainless steel vessels all share one requirement: a product that can’t tolerate contamination.
- Food processing: mixing tanks, storage vessels, and batch tanks for sauces, syrups, oils, and confectionery production
- Beverage manufacturing: fermentation tanks, bright tanks, and holding vessels for breweries, distilleries, and bottling lines
- Pharmaceutical and biotech: reactor and holding vessels where Ra requirements often exceed the standard sanitary threshold
- Dairy processing: silos, pasteurization equipment, and CIP-cleaned storage tanks
- Chemical processing: tanks where corrosion resistance and chemical compatibility matter as much as sanitation
What to Nail Down Before You Request a Quote
A few specification details separate a vessel that performs for decades from one that becomes a recurring problem:
- Capacity and configuration matched to actual production quantity, not a stock size
- Fittings and gaskets are compatible with both the product and the cleaning chemicals in use
- Heating and agitation requirements, since jacketed and mixing systems add design complexity
- Interior and exterior finish specs, documented separately, since they’re often different Ra targets
- Complete drawings up front, so the vessel fits the process the first time, not after a change order
- Delivery format shipped as a single unit or mounted on skids as part of a larger line
Why This Is a Fabrication Decision, Not Just a Material Decision
Choosing stainless steel only gets a facility halfway there. The finish, the welding, the passivation, and the fabricator’s ability to hold tolerances at every step determine whether a vessel performs for 20 years or becomes a compliance problem in year 3.
That’s the case for treating vessel fabrication as a single accountable process, not a chain of separate vendors passing a tank from a cutting shop to a welding shop to a polishing house. Schmidt Industrial Services fabricates stainless steel vessels for confectionery, chemical, biotech, and general food and beverage processing, backed by ASME U-Stamp and National Board R-Stamp certification.
Why Schmidt
Schmidt Industrial Services fabricates stainless steel vessels to ASME U-Stamp and National Board R-Stamp certification, with the welding, forming, machining, and finishing disciplines that determine whether a vessel meets spec all handled in-house, not split across separate vendors.
Our McCarter division has decades of experience building and repairing sanitary tanks for confectionery and food processing, and our team works from your drawings and specifications to build a vessel suited to your process, not a stock configuration adapted after the fact.
Read More
- 4 Things You Need to Know About Food-Grade Stainless Steel
- Carbon Steel vs Stainless Steel: Which Tank Material Is Best for Your Plant?
- The Ultimate Guide to Food Processing Equipment
If you’re specifying a custom stainless steel process tank or evaluating an existing vessel that’s due for replacement, contact our team or request a quote to discuss your project.